Non-contact dispensing
Jetting reduces unnecessary Z-axis motion between deposits.
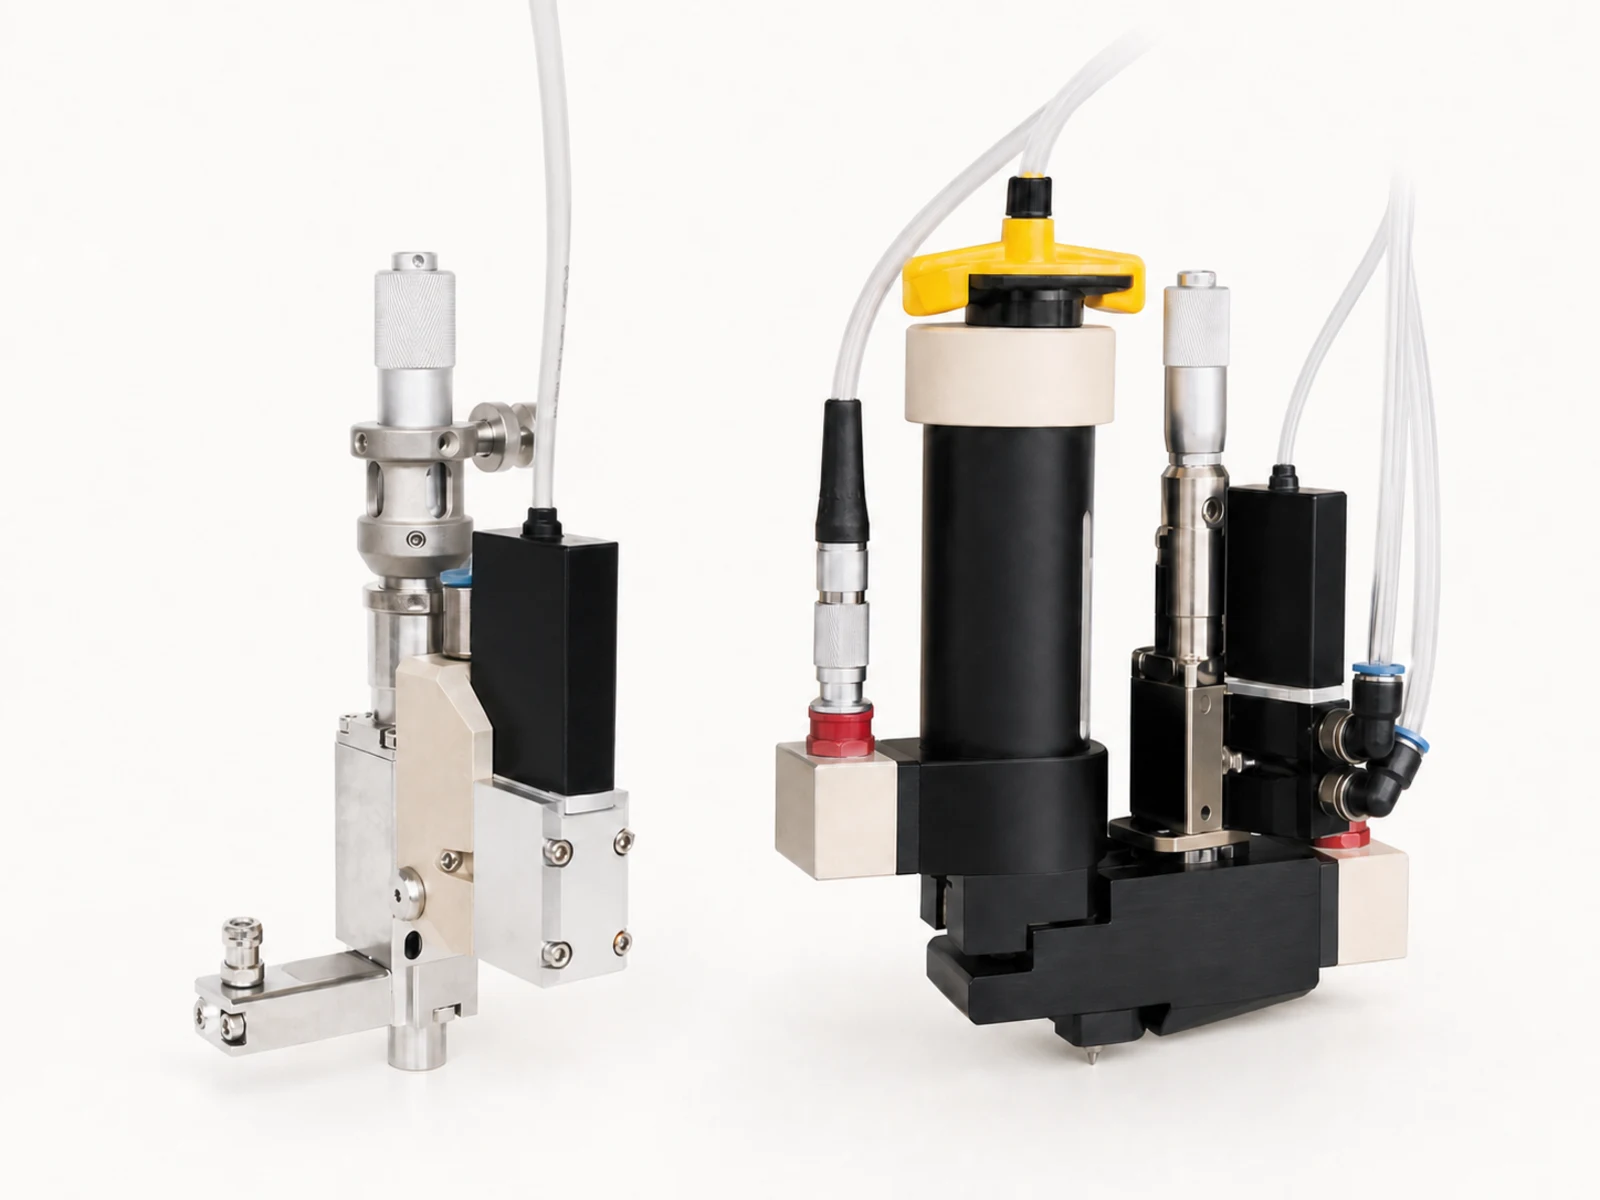
Pneumatic Jet Valve
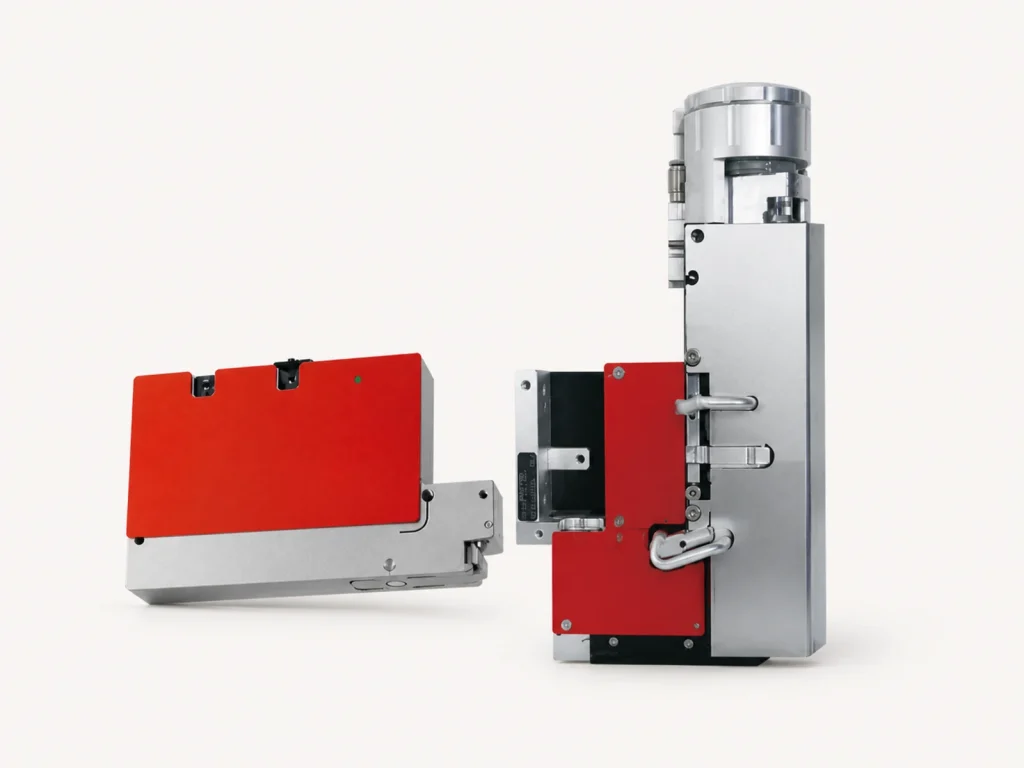
Aurexis Automation · AX-J6000/6200
Non-contact jetting for standard and heated adhesive processes.
Product overview
The AX-J6000/6200 family uses pneumatic actuation and solenoid timing for non-contact dispensing without a Z-axis touch-off move. AX-J6000 targets general adhesives, lubricants and inks; AX-J6200 adds a heated material path and 30 cc cartridge support for PUR and hot-melt processes.
Engineering advantages
Jetting reduces unnecessary Z-axis motion between deposits.
Select general-fluid or PUR/hot-melt configuration.
24 × 90 × 160 mm envelope supports benchtop platforms and integrated cells.
Modular valve components simplify removal and maintenance.
AX-J6000
Non-contact jetting for adhesive, lubricant, water-based solvent, polymer, ink and silicone.
AX-J6200
Heated fluid path and 30 cc cartridge for PUR and hot-melt adhesive.
Technical data
Model-level differences are separated below; shared and supplementary parameters follow the model cards.
| Jet mode | Non-contact pneumatic jetting |
|---|---|
| Series envelope | 24 × 90 × 160 mm |
| Minimum dot / volume | Approx. 0.3 mm; 0.002 µL |
| Frequency note | Overview states 250 Hz while the performance table states 200 Hz; engineering confirmation required |
Applications & options
Configure the heated fluid path for PUR or hot-melt adhesive.
Provides a compact heated material supply.
Match particle size, chemistry and target deposit.
Resources & support
Selection is confirmed against the workpiece, fluid, viscosity, deposit geometry and cycle requirement. Final specifications require engineering sign-off.
FAQ
Jetting can deposit without touching the workpiece and reduces repeated Z-axis travel.
The source overview states 250 Hz while the performance table states 200 Hz; 200 Hz is used here until engineering confirmation.
Particle size, abrasiveness and settling must be reviewed; the standard page lists particles below 20 µm.
Related equipment
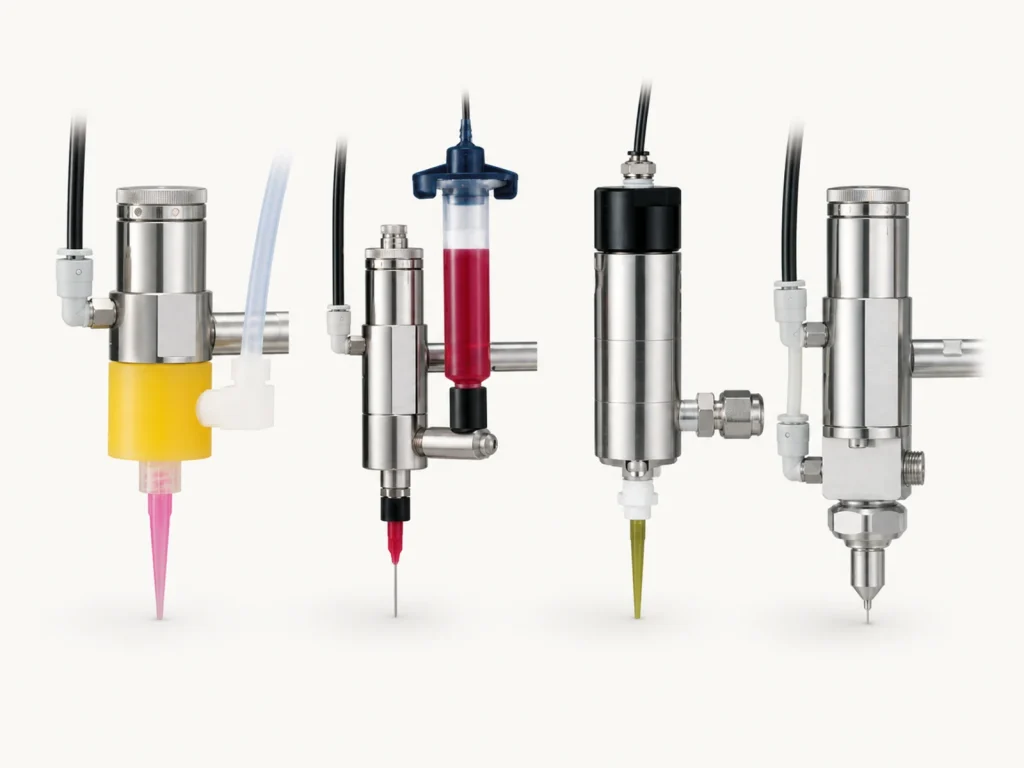
Ten pneumatic dispensing valves for dots, films, controlled beads, high pressure and precision mist patterns.
High-speed piezoelectric jet valve with 0.20 ms minimum pulse time and up to 1,200 Hz continuous dispensing frequency.
We will confirm equipment configuration, fixtures, process modules and line interfaces.